
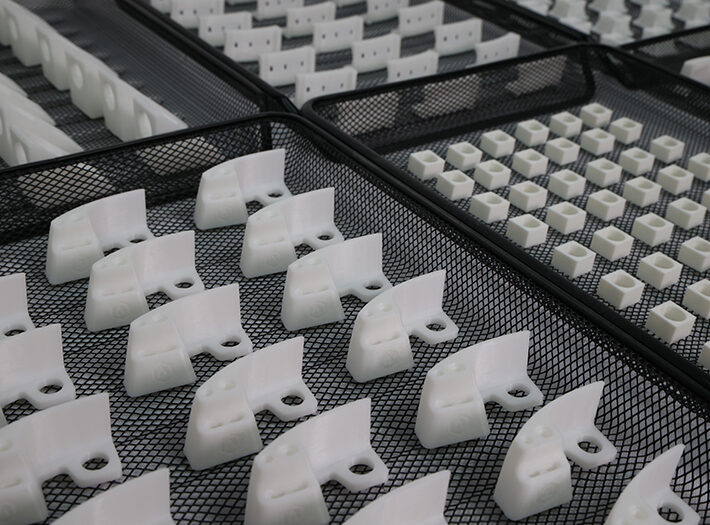
An Expert Blueprint for Scaling SLS-Like Workflows: Factory Onboarding, Sourcing, and Repeatable Production for Selective Laser Sintering Parts
Framework Overview
Think of this like a lookout map for bringin’ a brittle little prototype up to steady, high-volume runs—without losin’ your shirt. This framework lays out clear stages: material sourcing, process validation, operator onboarding, and iterative quality controls. I learned a heap runnin’ prints in a small Dayton, Ohio prototyping shop after the 2020 supply shocks; that reality check shaped how I scout 3d printer material and set up shop. The goal’s simple: predictable parts every shift, fewer rejects, and equipment that behaves—using sensible slicer settings, steady layer height, and clean nozzle maintenance where it matters.
Sourcing & Materials
Start by pickin’ materials that match function, not just price. For selective laser sintering-style runs, your polymer choice dictates build density, post-processing needs, and inspection cadence. When we shifted a batch to a more heat-stable filament, post-cure times dropped and dimensional drift tightened up. For everyday shop use, I recommend keepin’ a tested set of suppliers and a small inventory buffer to ride out delivery hiccups. Also, if you’re comparing filaments, look for consistent spool diameter and documented melt flow—those two things save more headaches than flashy specs.
Factory Onboarding Workflow
Onboardin’ operators ain’t about handin’ out a checklist and hopin’ for the best. Break training into hands-on stations: machine setup, slicing recipe, build prep, and QC checks. Train to tolerance bands not vague ideas. Use a simple build card per job that logs slicer profile, bed temp, and nozzle condition. That card becomes the one source for repeatability. Keep the language plain in those cards—no technical fluff—so a green hand can get a part right on the second go.
Operational Production Teardown
When I run an operational production teardown, I walk the full flow: material receipt → sample prints → dimensional checks → ramp to production. That teardown highlights where {main_keyword} hides and where {variation_keyword} creeps in. Measure things early: filament diameter variance, nozzle wear after X hours, and build plate flatness before each lot. Log those numbers and make go/no-go gates. This makes troubleshooting faster — you don’t hunt for ghosts when a batch tilts off spec.
Common Mistakes and Alternatives
Most shops trip up on two fronts: they under‑spec QC gates and they over‑complicate menus. Folks add too many variables to a slicer profile when a handful of stable settings would do. Fix that by standardizin’ profiles and lockin’ them in a versioned folder. Another mistake is skimpin’ on material checks—sketchy filament tolerances wreck throughput. Alternatives include outsourcing small runs to a trusted bureau or shifting to a hybrid workflow that pairs in-house printing with selective post-process sintering. Oh—and don’t forget basic maintenance routines that most ignore; do ’em weekly and you’ll dodge a lot of downtime.
Practical Checklist
Here’s a tight checklist to follow every production cycle: document spool lot, run a short calibration print, record nozzle hours, confirm bed adhesion with a standardized test coupon, and batch-accept parts with a dimensional gauge. Keep a lean logbook—simple entries beat complex forms every time.
Closing — Three Golden Rules
1) Metricize the handoffs: measure filament diameter variance, first-pass yield, and mean time between machine interventions. Those three metrics tell you if your process is stable. 2) Lock down your build recipes: maintain versioned slicer profiles and limit changes to controlled releases. 3) Train to tolerance, not task: teach people what an acceptable deviation looks like, then let them own fixes. Stick to those rules and your line’ll run smoother.
Final thought—real people run the kit, and practical systems keep ’em from burnin’ out. — Raise3D